
 Removing
(
Refitting
 )
 | This procedure is valid only for the 1.4 16v TJet - 155 HP version with C544 gearbox (M32). |
|
|
Removing
(
Refitting
)
|
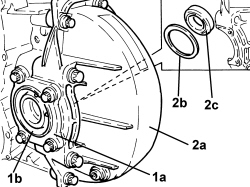  |
1. Undo the screws and remove the flange with the seal ring (1b). 2. Undo the screws and remove the differential internal casing support (2a), the scraper ring (2b) and the seal ring (2c). |
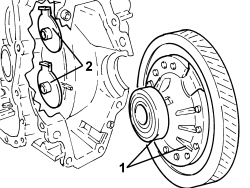  |
- Clean the contact surfaces between the differential internal casing support and the clutch casing thoroughly. 1. Remove the differential internal casing from its housing complete with bearing outer races. 2. Remove the lubrication oil ducts from the housings for the two layshafts. |
|
|
Refitting
(
Removing
)
- Fit the lubrication oil ducts in the housings for the two layshafts. - Apply LOCTITE 510 sealant to the entire matching surface between the differential internal casing housing and the clutch casing. - Fit the differential casing internal housing and support tightening the screws to the prescribed torque. The screw tightening must be made in three stages, as below described: approach the screws to 0.5 daNm; tighten the screws to 50% of the final required value, then tighten to 100% of the final required value.
|
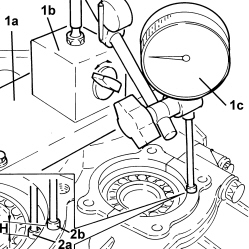  |
1. Fit a suitable steel plate (1a) on the clutch casing for the magnetic base (1b) with dial gauge (1c). 2. Measure the depth (H) between the surface of the gearbox (2a) and the surface of the bearing (2b). |
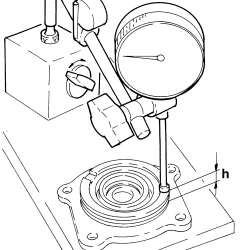  |
- Measure the depth (h) of the flange. |
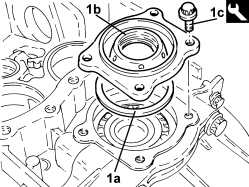  |
- Calculate the difference (H-h) to determine the size of the shim (S) for the scraper ring so that the clearance corresponds to the prescribed figure of 0.15 ± 0.05 mm. 1. Fit the new scraper ring (1a) and the new flange with the seal (1b) and tighten the screw (1c) to the prescribed torque.
|
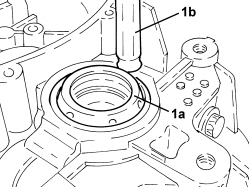  |
1. Fit a new seal ring (1a) on the differential internal casing support using a suitable drift (1b). |